
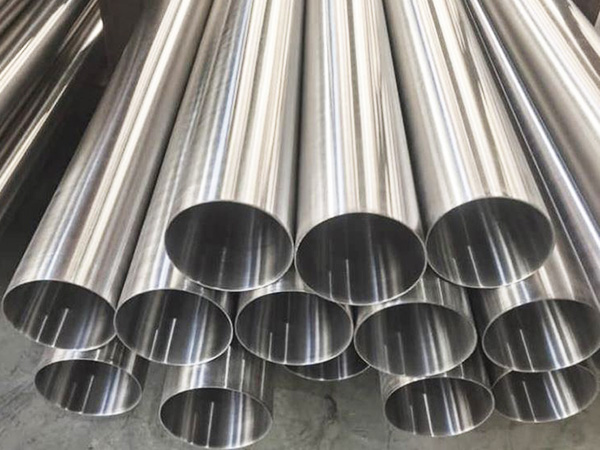
Among the stainless steel pipe grades available to industrial buyers, Grade 304 occupies a unique position. It is the most produced, most stocked, most widely specified austenitic stainless steel—serving as the baseline against which all other stainless grades are compared. Its balance of corrosion resistance, formability, weldability, and cost has made it the default specification for an enormous range of industrial, commercial, and architectural applications. Understanding what 304 stainless steel pipe actually delivers—its properties, its limitations, and the service conditions where it excels—helps engineers and procurement professionals specify it correctly and recognize when service conditions require upgrading to a higher-alloy alternative.
Chemical Composition and Microstructure
The defining chemistry of Grade 304 is approximately 18 percent chromium and 8 percent nickel—the composition that gave rise to the "18-8" designation that remains in common industrial usage. Chromium provides the passive oxide film that enables corrosion resistance; nickel stabilizes the austenitic microstructure that provides ductility, formability, and non-magnetic behavior. The balance of these elements creates a material that combines good corrosion resistance with excellent fabrication characteristics.
The ASTM A312 specification defines the chemistry limits for TP304 pipe: 18.0 to 20.0 percent chromium, 8.0 to 11.0 percent nickel, maximum 0.08 percent carbon (for the standard grade), maximum 2.0 percent manganese, maximum 1.0 percent silicon, maximum 0.045 percent phosphorus, and maximum 0.030 percent sulfur. These ranges provide the composition window within which the grade's properties are reliably achieved.
The austenitic microstructure that nickel stabilizes is face-centered cubic—a crystal structure that cannot be hardened through heat treatment but can be significantly strengthened through cold work. This structure remains stable across a wide temperature range, from cryogenic temperatures well below minus 196°C to elevated temperatures approaching 870°C for intermittent service. The non-magnetic character of austenitic stainless steel is a practical identification feature that helps distinguish 304 from ferritic and duplex grades in field applications.
Mechanical Properties
304 stainless steel pipe in the annealed condition, as typically supplied per ASTM A312, exhibits minimum mechanical properties that define its structural capability:
Yield strength: Minimum 205 MPa (30,000 PSI) — the stress at which permanent deformation begins
Tensile strength: Minimum 515 MPa (75,000 PSI) — the maximum stress before rupture
Elongation: Minimum 35 percent in 50 mm — the ductility that enables forming and indicates resistance to brittle fracture
Hardness: Maximum 92 HRB (Brinell 201) — indicating the relatively soft, readily machinable condition of annealed austenitic stainless
These properties reflect the annealed condition that ASTM A312 requires for finished pipe. Cold working can significantly increase yield and tensile strength—reaching 60,000 to 80,000 PSI yield in heavily cold-drawn conditions—but at the cost of reduced ductility. For pressure-containing applications, the annealed condition is standard because it provides the best combination of strength, ductility, and corrosion resistance.
The modulus of elasticity of 304—approximately 193 GPa (28,000 ksi)—is lower than carbon steel's 200 GPa. This difference affects deflection calculations for structural applications and requires attention when substituting stainless for carbon steel in load-bearing designs. The thermal expansion coefficient of 304 (approximately 16.5 µm/m°C from 0 to 100°C) is significantly higher than carbon steel's 12.1 µm/m°C, requiring thermal expansion accommodation in piping system design to avoid excessive stress at supports and connections.
Corrosion Resistance Characteristics
Atmospheric and Fresh Water Corrosion
Grade 304 provides excellent resistance to atmospheric corrosion in rural, urban, and industrial environments. The passive chromium oxide film forms spontaneously in oxidizing conditions and repairs itself when mechanically damaged, providing continuous protection without the need for coatings or maintenance. In fresh water service, 304 resists corrosion indefinitely under normal conditions. These characteristics make it the standard specification for indoor plumbing, architectural handrails, food contact surfaces, and general-purpose corrosion-resistant service.
Organic Acid and Chemical Resistance
304 stainless steel pipe provides good resistance to many organic acids at moderate concentrations and temperatures—acetic acid, formic acid, citric acid, and other acids encountered in food processing and pharmaceutical manufacturing. It also resists many alkaline solutions and neutral salts effectively. This corrosion profile makes 304 the standard grade for dairy, brewery, food processing, and pharmaceutical process piping where the media are organic and chloride-free.
Where 304 Fails: Chloride Environments
The critical limitation of Grade 304 is its susceptibility to chloride-induced corrosion. Chloride ions penetrate the passive film, initiating pitting corrosion—localized attack that can perforate pipe walls rapidly in concentrated chloride environments. Crevice corrosion—attack in shielded areas where chlorides concentrate—occurs at gasket surfaces, bolted joints, and deposits where stagnant conditions enable chloride concentration.
Even trace chlorides can cause problems. Coastal atmospheric deposition carries chlorides that can initiate pitting on 304 surfaces exposed to marine air. Cooling water systems with even modest chloride content can cause pitting in heat exchanger tubing. Cleaning solutions containing chlorides—bleach, chlorinated cleaners—can damage 304 surfaces if contact is prolonged or concentrated. For any application where chloride exposure is possible, Grade 316 with its molybdenum addition provides the necessary pitting resistance improvement.
Stress Corrosion Cracking
Austenitic stainless steels including 304 are susceptible to chloride stress corrosion cracking (SCC) under specific conditions: tensile stress, chloride presence, and elevated temperature (typically above 60°C). This failure mode can cause sudden cracking through the pipe wall without significant visible warning, creating leak or rupture risk in pressure-containing systems. Applications involving chlorides at elevated temperatures with tensile stress—such as hot chloride-bearing process streams or insulated piping where chlorides leach from insulation under temperature—should evaluate duplex grades that resist SCC, rather than relying on 304.
Temperature Capability
304 stainless steel pipe provides service across a broad temperature range that contributes to its versatility. At cryogenic temperatures, the austenitic microstructure retains toughness that ferritic and martensitic steels lose. Grade 304 maintains significant impact toughness at minus 196°C (liquid nitrogen temperature) and below, making it suitable for cryogenic process piping handling liquefied gases.
At elevated temperatures, 304 provides useful strength and oxidation resistance to approximately 870°C for intermittent service and 925°C for continuous service. However, prolonged exposure in the 425 to 900°C range causes sensitization—chromium carbide precipitation at grain boundaries that depletes chromium from the adjacent matrix, reducing the grain boundary corrosion resistance. For applications involving sustained operation in this temperature range, the stabilized grades (TP321, TP347) or the low-carbon variant (TP304L) should be specified.
The ASME BPVC Section II Part D provides allowable stress values for 304 across the full temperature range, with values decreasing progressively at elevated temperatures. Piping system design per ASME B31.3 uses these allowable stresses to calculate minimum required wall thickness for pressure-containing applications.
304L: The Low-Carbon Variant for Welded Construction
For welded 304 stainless steel pipe, the low-carbon variant TP304L should be the standard specification. With maximum carbon content of 0.030 percent (versus 0.08 percent for standard TP304), the L-grade minimizes the chromium carbide formation that causes sensitization during welding. The reduced carbon content has minimal effect on mechanical properties in the annealed condition—yield strength is marginally lower—and no practical effect on corrosion resistance in normal service.
The practical consequence of specifying TP304L rather than TP304 for welded pipe is that the heat-affected zone retains its corrosion resistance after welding, eliminating the need for post-weld solution annealing to restore corrosion properties. This simplifies fabrication, reduces cost, and improves the reliability of welded stainless piping systems. For seamless pipe that will not be welded, standard TP304 may provide slightly higher strength, but the practical difference is negligible for most applications.
Many suppliers stock TP304L as their standard 304-grade product because it serves both welded and seamless applications effectively. When procurement specifications list TP304 without the L designation, the delivered material may be either grade—creating uncertainty about post-weld corrosion resistance. Specifying TP304L explicitly eliminates this ambiguity.
Applications Where Grade 304 Excels
Food, Beverage, and Pharmaceutical Processing
The food and pharmaceutical industries represent the largest single application category for 304 stainless steel pipe. The combination of corrosion resistance to organic media, hygienic surface characteristics, non-toxic non-reactive behavior, and cleanability makes 304 the standard material for process piping, equipment, and storage in these industries. The 2B or polished surface finishes typically specified provide the smooth, easily cleaned surfaces that hygienic standards require.
Chemical Processing (Non-Chloride)
For chemical process streams involving organic acids, alkaline solutions, and neutral salts at moderate temperatures, Grade 304 provides cost-effective corrosion resistance. Applications involving chlorides, reducing acids at high concentration, or elevated-temperature chloride service require Grade 316 or higher-alloy alternatives.
Architectural and Structural Applications
Grade 304 serves architectural handrails, railings, column covers, and decorative elements where atmospheric corrosion resistance and aesthetic appearance matter. The material's formability enables the bent and formed shapes that architectural designs require. For coastal or marine architectural applications, Grade 316 provides better resistance to chloride deposition from marine atmospheres.
Cryogenic and Low-Temperature Service
The toughness retention of austenitic stainless steel at cryogenic temperatures makes Grade 304 suitable for liquefied gas handling, refrigeration systems, and cold-climate process piping where carbon steel would become brittle. For the most demanding cryogenic applications, the impact testing requirements of ASTM A333 may apply, and 304's performance should be verified through testing at the design temperature.
Specification and Procurement Guidance
Effective procurement of 304 stainless steel pipe requires complete specification of the elements that define the material:
ASTM specification: A312 for seamless or welded austenitic pipe; A358 for large-diameter EFW pipe; A409 for welded pipe in corrosive high-temperature service
Grade designation: TP304 or TP304L, with UNS number S30400 or S30403 for precise specification
Manufacturing method: Seamless (SMLS) or welded (ERW, EFW) as the application requires
Size and schedule: NPS diameter and schedule number or wall thickness
Surface finish: Annealed and pickled, 2B, polished (240 grit, 320 grit, etc.) as application requires
End preparation: Plain end, beveled for welding, threaded, or grooved
Testing requirements: Hydrostatic test, non-destructive examination if required beyond standard A312 requirements
Certification: Mill Test Report per EN 10204 Type 3.1 or 3.2 as project requirements dictate
Mill Test Reports should document actual heat chemistry against A312 limits, mechanical properties (yield, tensile, elongation), and confirmation that the material was supplied in the annealed condition. For critical applications, consider specifying PMI (Positive Material Identification) at receiving inspection to verify that delivered material is actually Grade 304 rather than a misidentified grade.
Conclusion
304 stainless steel pipe provides the corrosion resistance, fabrication versatility, and cost-effectiveness that make it the default specification for a vast range of industrial applications. Its 18-8 chemistry delivers reliable performance in atmospheric, fresh water, organic acid, and food-grade service. The austenitic microstructure provides excellent ductility, toughness from cryogenic to elevated temperatures, and weldability that supports complex fabrication.
The critical limitation—chloride susceptibility—must be recognized and addressed through grade selection. Applications involving chloride exposure should specify Grade 316 or higher-alloy alternatives rather than accepting the premature failure risk that 304 creates in chloride environments. For welded construction, TP304L should be the standard specification to prevent sensitization and preserve heat-affected zone corrosion resistance.
Procurement teams that specify complete requirements, verify material compliance through MTR review, and conduct PMI at receiving inspection consistently achieve reliable stainless piping installations. The investment in specification discipline and material verification protects against the substitution errors and specification mismatches that can compromise corrosion-resistant piping performance. For applications requiring 304 stainless steel pipe, sourcing from a manufacturer who provides certified material, complete documentation, and consistent quality ensures the material performance that engineering designs depend upon.
FAQ
Q: What is the maximum temperature for 304 stainless steel pipe?
A: Grade 304 provides useful service to approximately 870°C for intermittent exposure and 925°C for continuous oxidation resistance. However, prolonged exposure in the 425 to 900°C range causes sensitization (chromium carbide precipitation) that reduces intergranular corrosion resistance. For sustained high-temperature service in this range, specify TP321, TP347 (stabilized grades), or TP304L (low-carbon variant) to prevent sensitization.
Q: Should I specify 304 or 304L for welded stainless pipe?
A: Specify TP304L for any welded construction. The low-carbon content (max 0.030%) minimizes chromium carbide precipitation during welding, preserving corrosion resistance in the heat-affected zone without requiring post-weld solution annealing. The mechanical property difference between TP304 and TP304L in the annealed condition is negligible for most applications.
Q: Is 304 stainless steel pipe magnetic?
A: In the fully annealed condition, Grade 304 is essentially non-magnetic due to its austenitic microstructure. However, cold working—through forming, bending, or cold drawing—can transform some austenite to martensite, creating mild magnetic response in heavily worked areas. This partial magnetism does not indicate a material defect or grade mismatch; it is a normal response of austenitic stainless to cold work.
Q: Can 304 stainless steel pipe be used for seawater applications?
A: No. Seawater chloride concentration causes rapid pitting and crevice corrosion in Grade 304. For seawater service, specify Grade 316 as a minimum, with duplex grades (2205, 2507) providing superior performance for long-term or critical seawater applications. Even Grade 316 may experience localized corrosion in stagnant seawater conditions where chlorides concentrate.
Q: How do I verify that delivered pipe is actually Grade 304?
A: Request Mill Test Reports per EN 10204 Type 3.1 or 3.2 that document actual chemistry against ASTM A312 TP304 limits. For critical applications, conduct Positive Material Identification (PMI) using a handheld X-ray fluorescence (XRF) analyzer at receiving inspection. PMI verifies chromium and nickel content on the actual pipe surface, detecting misidentified or substituted material that MTR documentation alone cannot reveal.
References
ASTM International. (2024). ASTM A312/A312M-24: Standard Specification for Seamless, Welded, and Heavily Cold Worked Austenitic Stainless Steel Pipe. West Conshohocken, PA.
American Society of Mechanical Engineers. (2023). ASME BPVC Section II Part D: Materials Properties. New York, NY.
ASM International. (2023). ASM Specialty Handbook: Stainless Steels. Materials Park, OH.
Sedriks, A.J. (2023). Corrosion of Stainless Steels (2nd ed.). New York, NY: John Wiley & Sons.
American Society of Mechanical Engineers. (2022). ASME B31.3: Process Piping. New York, NY.